

 ENG
 中文简体
 русский
 Français
 Español
 日本語
 عربى
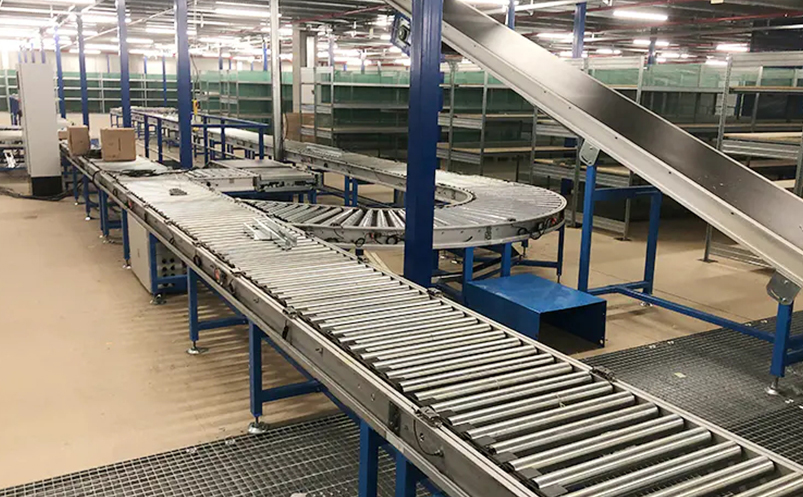
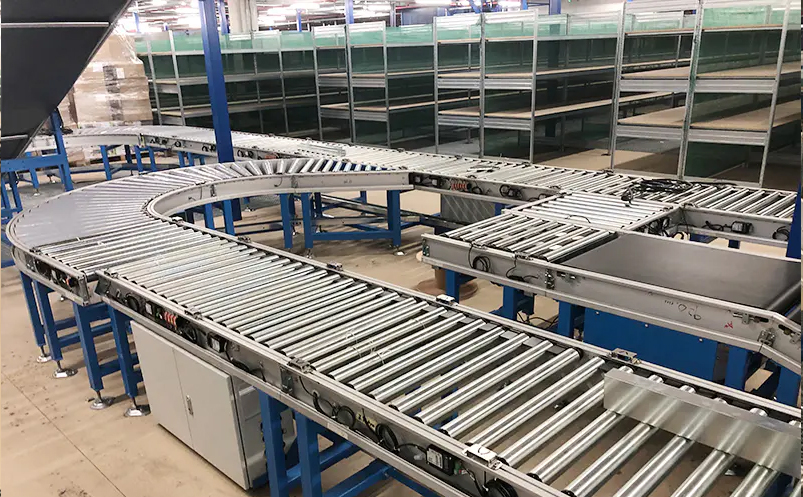
Custom heavy duty chain pallet conveyor integrated with 4 pneumatic lifting transfer stations to realize 90-degree bidirectional diversion, optimized for new energy and automotive automatic assembly lines.
Wuxi Huiqian Logistics Machinery Manufacturing Co.,LTD new conveyor line project designed according to customer's demand—heavy-duty chain pallet conveyor system equipped with four sets of pneumatic lifting transfer units, enabling stable double-side pallet diversion on automated production lines. The integrated conveyor solution addresses the growing demand for flexible pallet sorting and lane switching within heavy-load assembly workshops.
This heavy-duty chain conveyor adopts thick welded carbon steel frame and double-row chain driving structure, designed for long-term continuous transportation of heavy pallets and tooling fixtures. The four built-in pneumatic lifting transfer stations serve as core switching modules along the main line. When a pallet arrives at a target station, air cylinders lift the entire chain platform, separating the pallet from the main conveying surface. The transverse chain mechanism then moves the workpiece to left or right branch conveyor lines, completing automatic 90-degree direction change and material diversion.
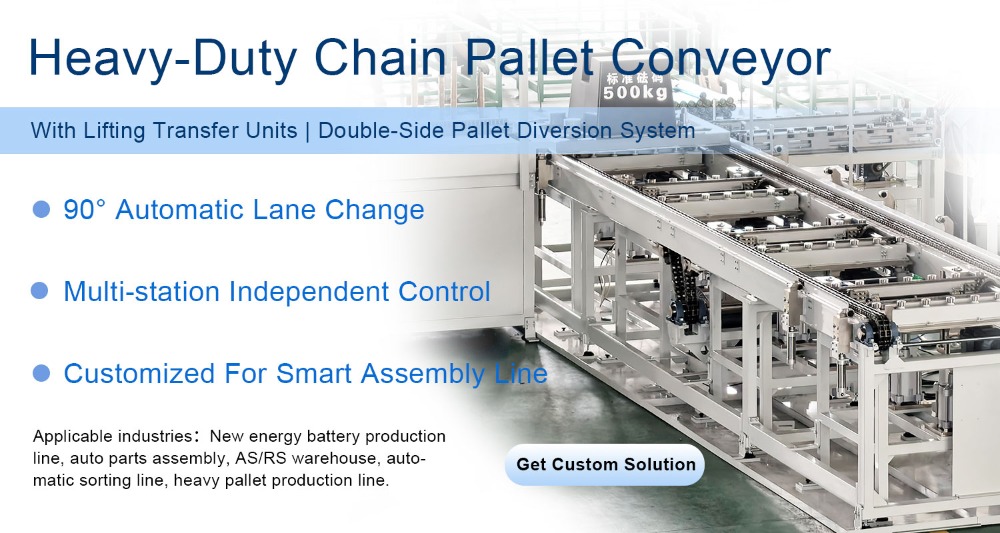
Each lifting transfer unit uses guide pillar synchronous guiding structure to guarantee vertical and stable lifting movement, effectively preventing platform tilt under heavy load conditions. The air source pressure for cylinder operation is adjustable within 0.4~0.7 MPa. Operators can tune the pressure according to actual workpiece weight to balance lifting force and reduce mechanical impact. All stations support independent control and can work separately or synchronously, matching flexible production tact of modern smart factories.
The whole conveyor system supports PLC and photoelectric sensor interlock, realizing automatic signal interaction with upstream and downstream equipment. Modular assembly design simplifies on-site installation, maintenance and later line expansion. The conveyor can be customized in length, width and load capacity to fit different workshop layouts. Typical application industries include new energy battery assembly, automotive component production, automated warehousing and heavy goods packaging.
‘Many of our clients need multi-point pallet sorting on one main conveyor line instead of single-direction transfer’, said the engineering manager of the manufacturer. “This integrated heavy-duty chain conveyor with multiple lifting transfer stations removes the limitation of traditional single-station diverters. Factories can build compact diverting lines without extra large space occupation, lowering overall workshop transformation investment.”
Compared with separated transfer machines, this combined line reduces intermediate transition gaps and improves operation stability. The heavy-duty frame and wear-resistant chain components ensure long service life under 24-hour continuous operation. Adjustable foot cups are equipped for ground leveling to adapt uneven factory floors.
The pallet handling system is available for global industrial buyers, supporting non-standard customization based on workpiece size, load weight and production process requirements. The manufacturer provides full services including solution design, factory pre-test, on-site installation guidance and after-sales technical support for overseas automation projects.
Wuxi Huiqian specializes in designing and manufacturing customized conveying and pallet transfer equipment, including roller conveyors, chain conveyors, pneumatic lifting transfer machines and automated sorting systems. It supplies material handling equipment for factories across automotive, new energy and logistics sectors, exporting automation solutions worldwide.