

 ENG
 中文简体
 русский
 Français
 Español
 日本語
 عربى
For factories and distribution centers investing in vertical material transport, selecting between chain vertical lifting conveyor and wire rope vertical lifters directly affects operational stability, maintenance schedules and long-term production costs. Both types of vertical lifting equipment serve pallet transfer, cross-floor workpiece transportation and production line connection, yet they feature distinct mechanical traits and suitable working conditions.
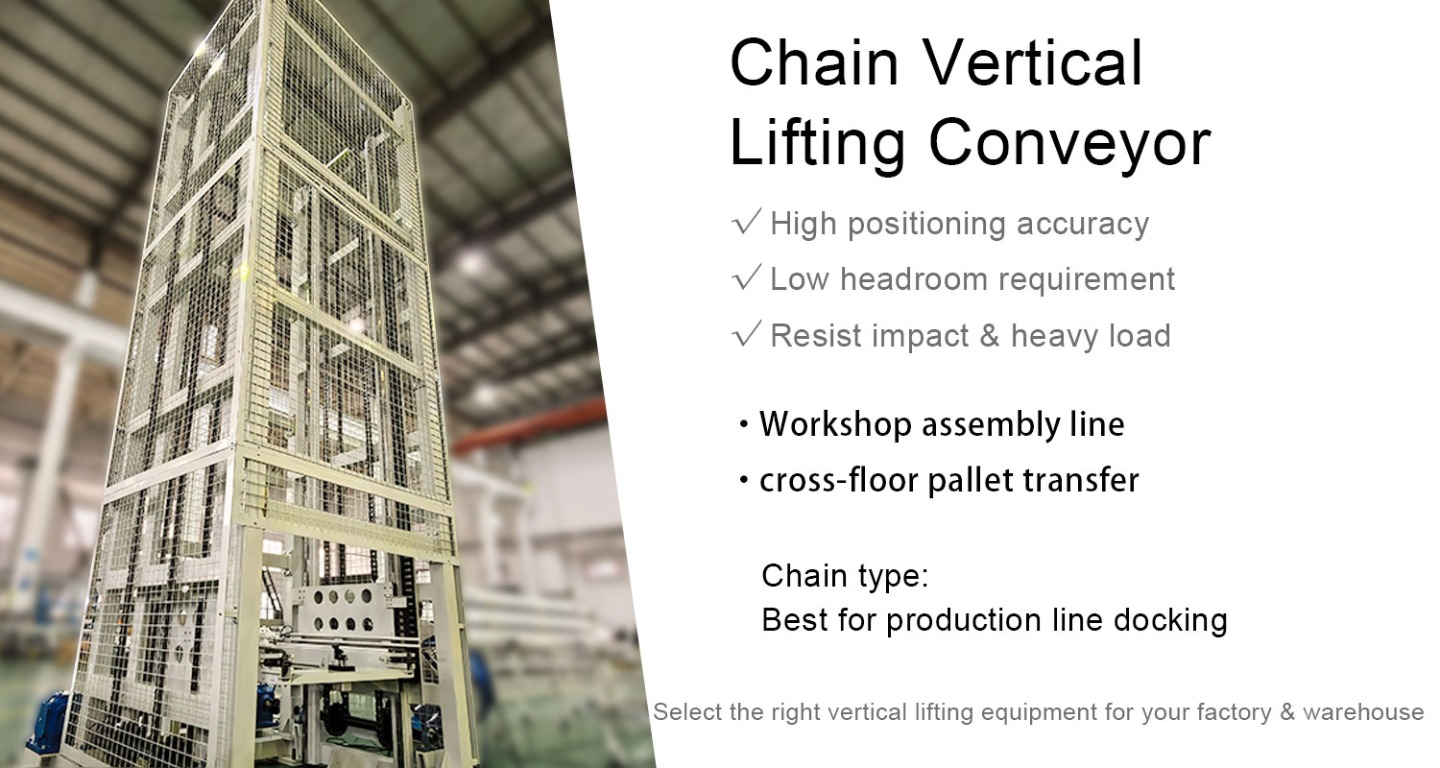
Chain vertical lifting conveyor adopt hardened load chains as the traction medium. The most prominent advantage is minimal elastic elongation during repeated lifting cycles. Multiple chains maintain excellent synchronization, keeping the cargo platform level and delivering high positioning accuracy. This characteristic makes chain lifts ideal for frequent start-stop operation and production line integration. The equipment structure is compact and requires low headroom, so it fits workshops with limited ceiling height. In dusty environments and applications with sharp-edged heavy workpieces, alloy chains show strong impact and crush resistance. Operators can visually inspect chain wear conveniently during daily checks. The typical recommended lifting height for chain vertical lifting conveyor stays within 20 meters.
On the other hand, chain vertical lifting conveyor generate relatively higher running noise. Continuous fatigue wear may cause sudden chain failure without clear early warning, so regular lubrication and periodic measurement of chain elongation are mandatory. The whole machine also carries heavier self-weight, which should be considered during civil foundation design. Common application scenarios include workshop inter-floor transfer, speed chain production line matching, auto parts assembly and medium-sized warehouse pallet conveying.
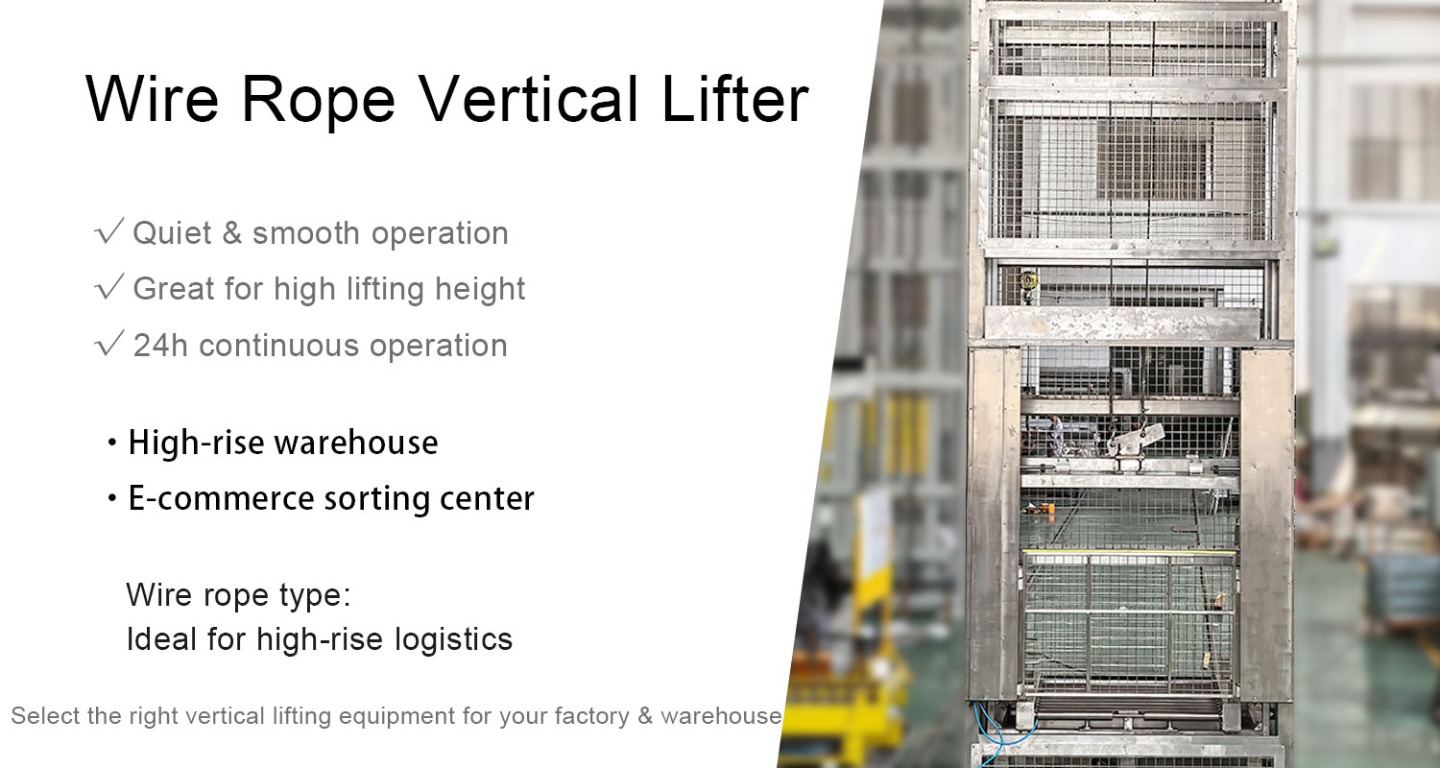
Wire rope vertical lifters utilize multi-strand steel wire rope for lifting transmission. Their core strengths lie in light traction component weight, smooth motion and low operating noise. For lifting heights over 20 meters, wire rope solutions provide better cost performance and faster lifting speed. Damage develops gradually: broken steel wires appear progressively, giving maintenance teams enough warning window to replace components before safety incidents. Under equal load capacity, wire rope lifting systems consume less driving power and offer reliable heat dissipation, supporting 24-hour continuous multi-shift operation for large automated logistics systems. Individual wire rope replacement is simpler and cheaper than replacing a full chain set.
The limitations of wire rope lifters also require attention. Steel wire ropes will stretch slightly under tension, so re-leveling adjustment is needed after a period of operation. Improper rope winding on the drum may lead to rope tangling and abrasion. Sharp corners on cargo can cut wire strands, and trapped dust inside rope strands creates hidden internal wear. In addition, the winding drum occupies vertical space, demanding higher headroom and making it less suitable for low-ceiling plants. It is widely adopted in high-rise automated warehouses, large distribution centers and e-commerce sorting facilities.
To simplify selection: choose chain vertical lifting conveyor if your factory has low ceiling height, frequent pallet circulation or needs direct docking with assembly production lines. Wire rope vertical lifters are preferred for high lifting strokes, continuous round-the-clock operation and low-noise requirements. The final equipment configuration should be confirmed after evaluating lifting height, load weight, working cycle, site space and environmental conditions.
Wuxi Huiqian Logistics Machinery has accumulated 15 years of experience in designing and manufacturing logistics conveying and lifting equipment. The engineering team delivers fully non-standard custom vertical lifting conveyor, adjusting traction mode, platform dimension, load capacity and safety protection systems to match unique workshop layouts and production workflows for global industrial clients.